Explore how new software development is assessed using the existing operating sequence, field signals and operator knowledge.
Missing program backups are a common issue when machine automation needs upgrading. The work possible is defined by the machine’s current condition, available documents, field connections and required functions. At Enopan, we assess the scope for developing new PLC and HMI software by examining the operating sequence of machines without backups.
First identify which file is missing
“No program” can mean different things. The PLC project file may be missing, the HMI screen project may be unavailable or an existing backup may not be linked to a known machine. Drive parameters and electrical drawings are separate documents. Each is matched to its device during the initial review.
A working application in a device does not mean its editable source project is available. The content and reuse potential of a backup obtained from a device vary by product. Versions and usage conditions of files available from the manufacturer or previous project team should be clarified at this stage.
A running machine is an important source of information
If the machine runs, starting, automatic cycles, manual operation and normal stopping can be observed. Operator commands, the sensor signals that trigger subsequent movements and the settings used are recorded. This describes the behaviour the new software must support.
Ask about conditions that occur rarely during production too. Product changes, interrupted processes, the state after a power outage or incorrect sensor signals may not be understood from watching a normal cycle alone. Operator and maintenance team knowledge is assessed alongside available documents.
How does the assessment proceed if the machine is not running?
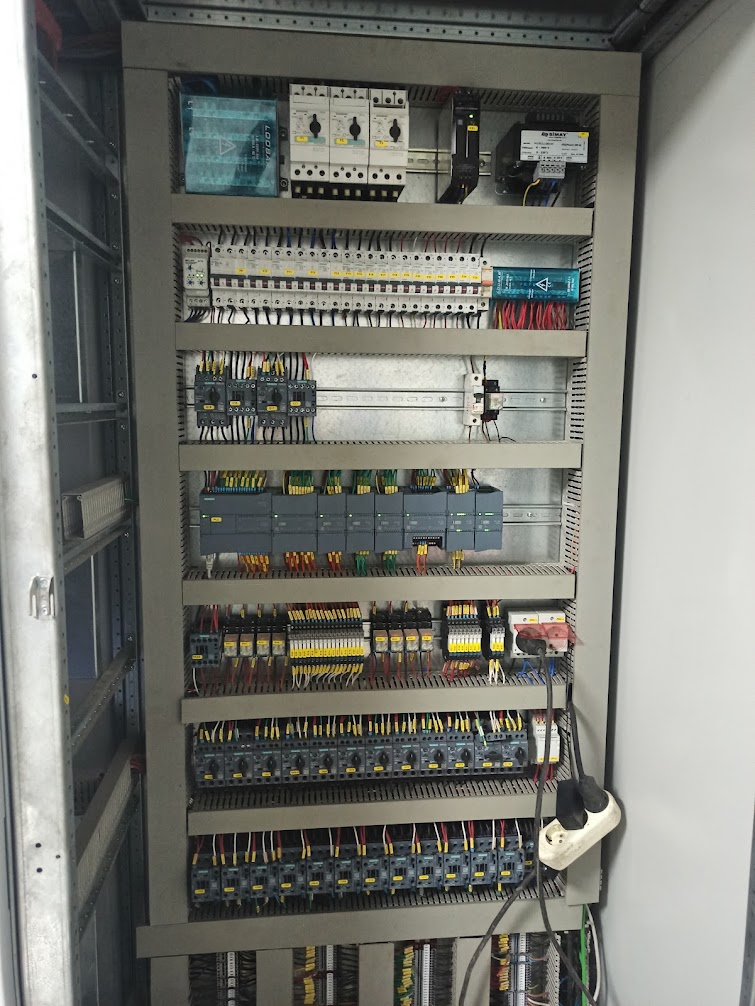
For a non-running machine, electrical drawings, equipment labels, field signals, old screenshots and operating documents become more important. The roles of existing PLCs, HMIs, drives and auxiliary control devices are established. The scope should not be based solely on PLC replacement before identifying which device performs each function.
Documents are also checked against the machine’s latest configuration. A motor added later or a replaced sensor may be missing from an old drawing. Uncertain operating steps remain explicitly unresolved in the sequence until technical review clarifies them; software delivery is not planned by guessing machine behaviour.
An operating sequence is prepared for the new software
Sensors, motors, valves and other outputs are matched to their functions. The description states which conditions issue each command, which settings operators can change and what triggers an alarm. Existing functions to retain and functions to add are listed separately.
| Information group | Contents |
|---|---|
| Machine behaviour | Automatic cycles, manual commands and process transitions |
| Field connections | Sensors, motors, valves and available feedback |
| Operator screen | Commands, statuses, settings and alarm descriptions |
| Acceptance scope | Which function will be checked on site and against what result |
Is software enough, or are hardware changes also required?
The condition of the existing PLC and HMI, available software tools, connection capabilities and required inputs/outputs are assessed together. Existing hardware may be retained in some projects; some machines may require changes to the screen, controller or panel connections. This distinction is made after the initial review.
The machine’s mechanical functions and required protection arrangements are also part of the assessment. Developing new control software does not automatically verify the suitability of all field equipment. Testing and intervention are planned alongside the relevant equipment.
How are commissioning and file handover planned?
The prepared program is compared on site against the defined operating sequence. Field signals, process transitions, manual and automatic commands and alarm notifications are checked. Production downtime that can be planned provides initial information for scheduling implementation and tests.
For Enopan projects, PLC/HMI program backups, electrical drawings, an operating manual and operator training are part of standard handover. Updating backups after the final change and identifying the version running on the machine allows later maintenance or development to be assessed using the same files.
Start with the information available for your machine
Share the machine’s function, whether it runs and the change required. We can assess the scope for new software using PLC/HMI labels, panel photographs and any old documents.