Machine automation brings sensors, motors, drives and the operator panel together according to the machine operating sequence. At Enopan, we develop PLC and HMI software for presses, cutting, filling, packaging and conveying machines. For new installations and existing machine automation retrofits, we engineer panels, drive connections, communications and commissioning according to the machine equipment.
Screen and control panel examples from our work
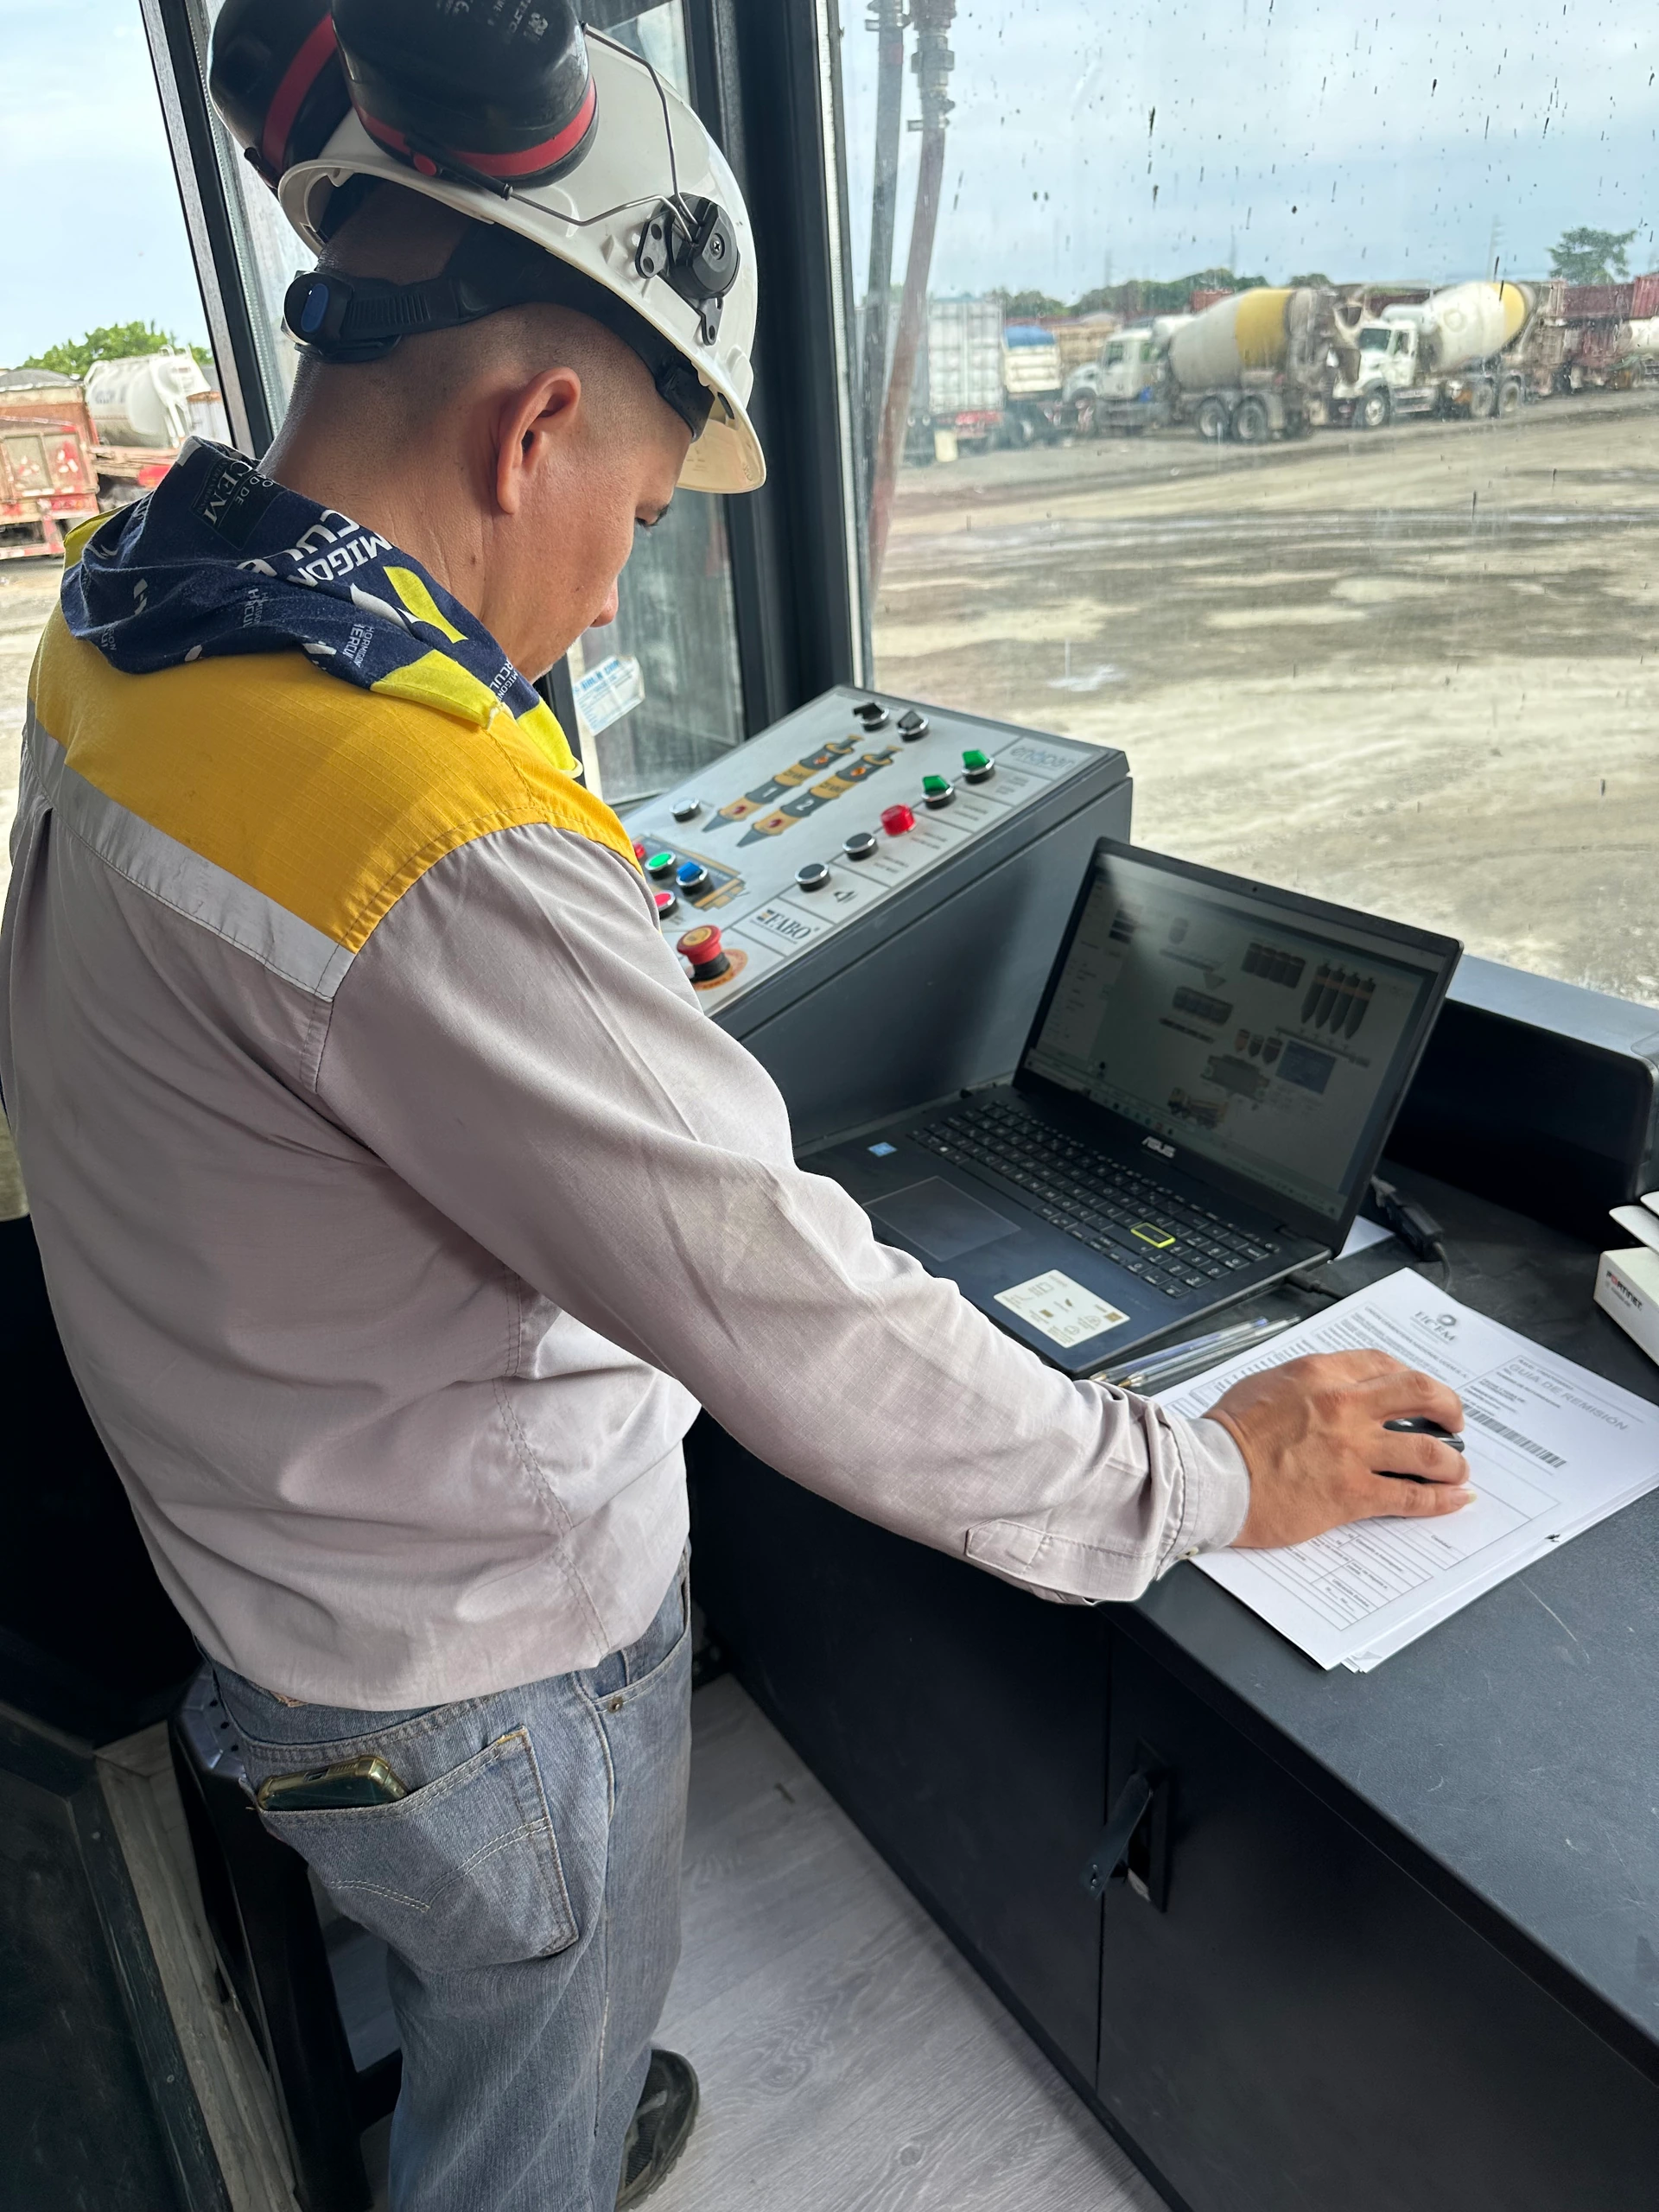
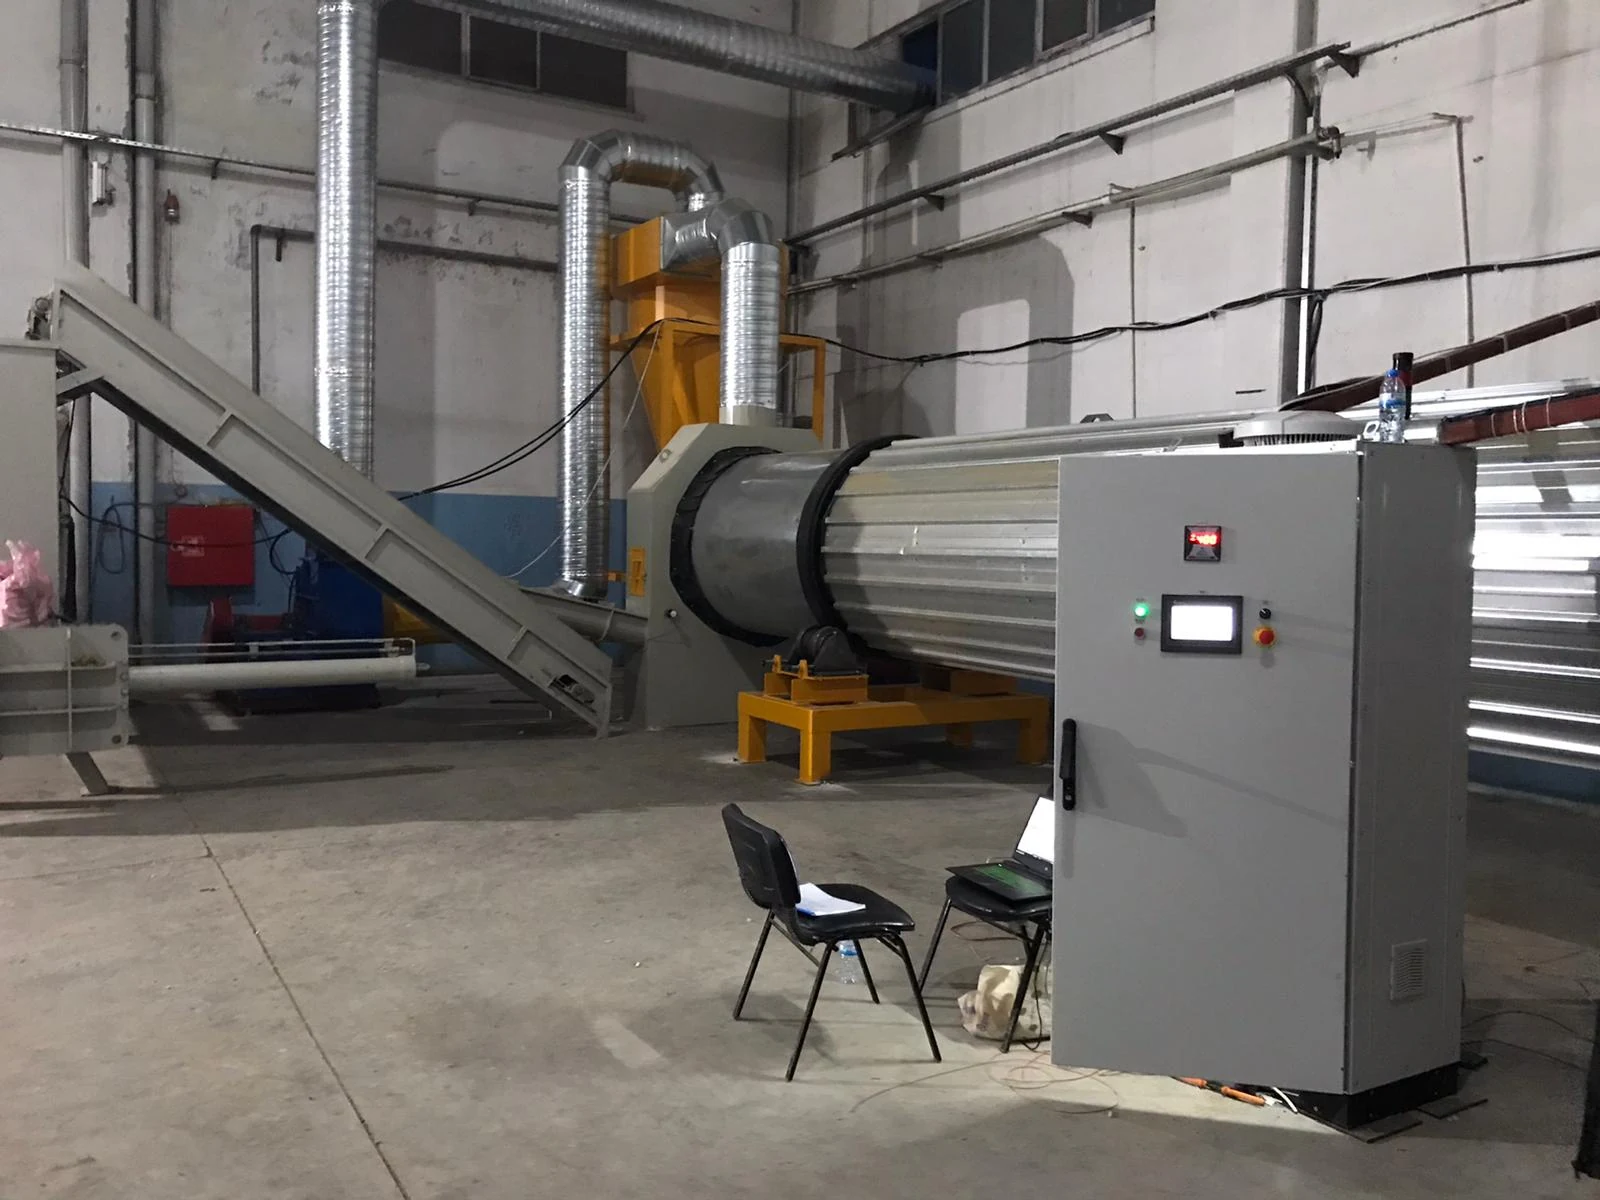
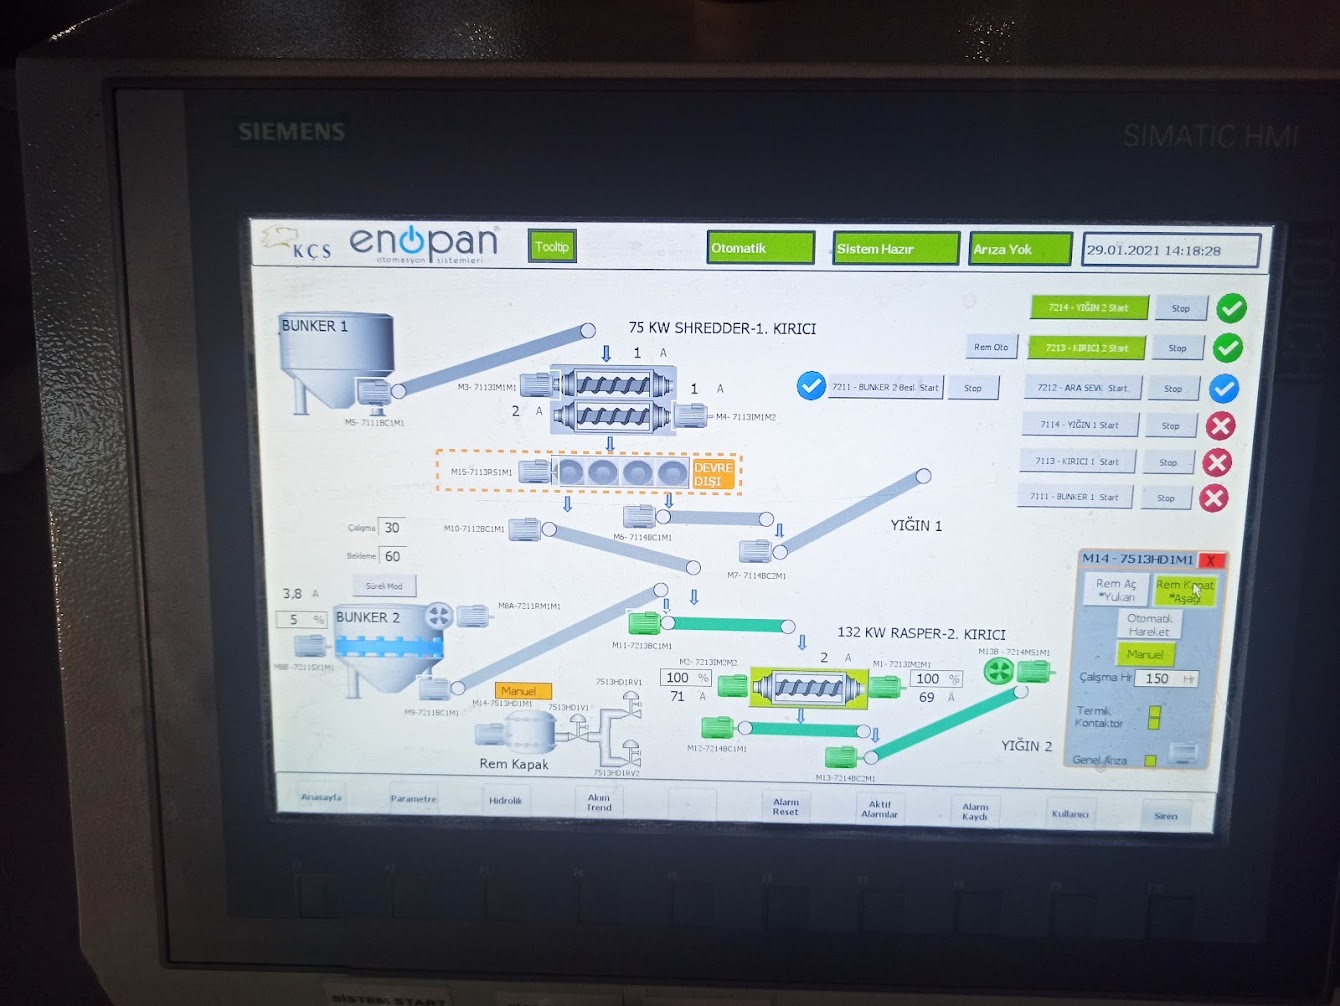
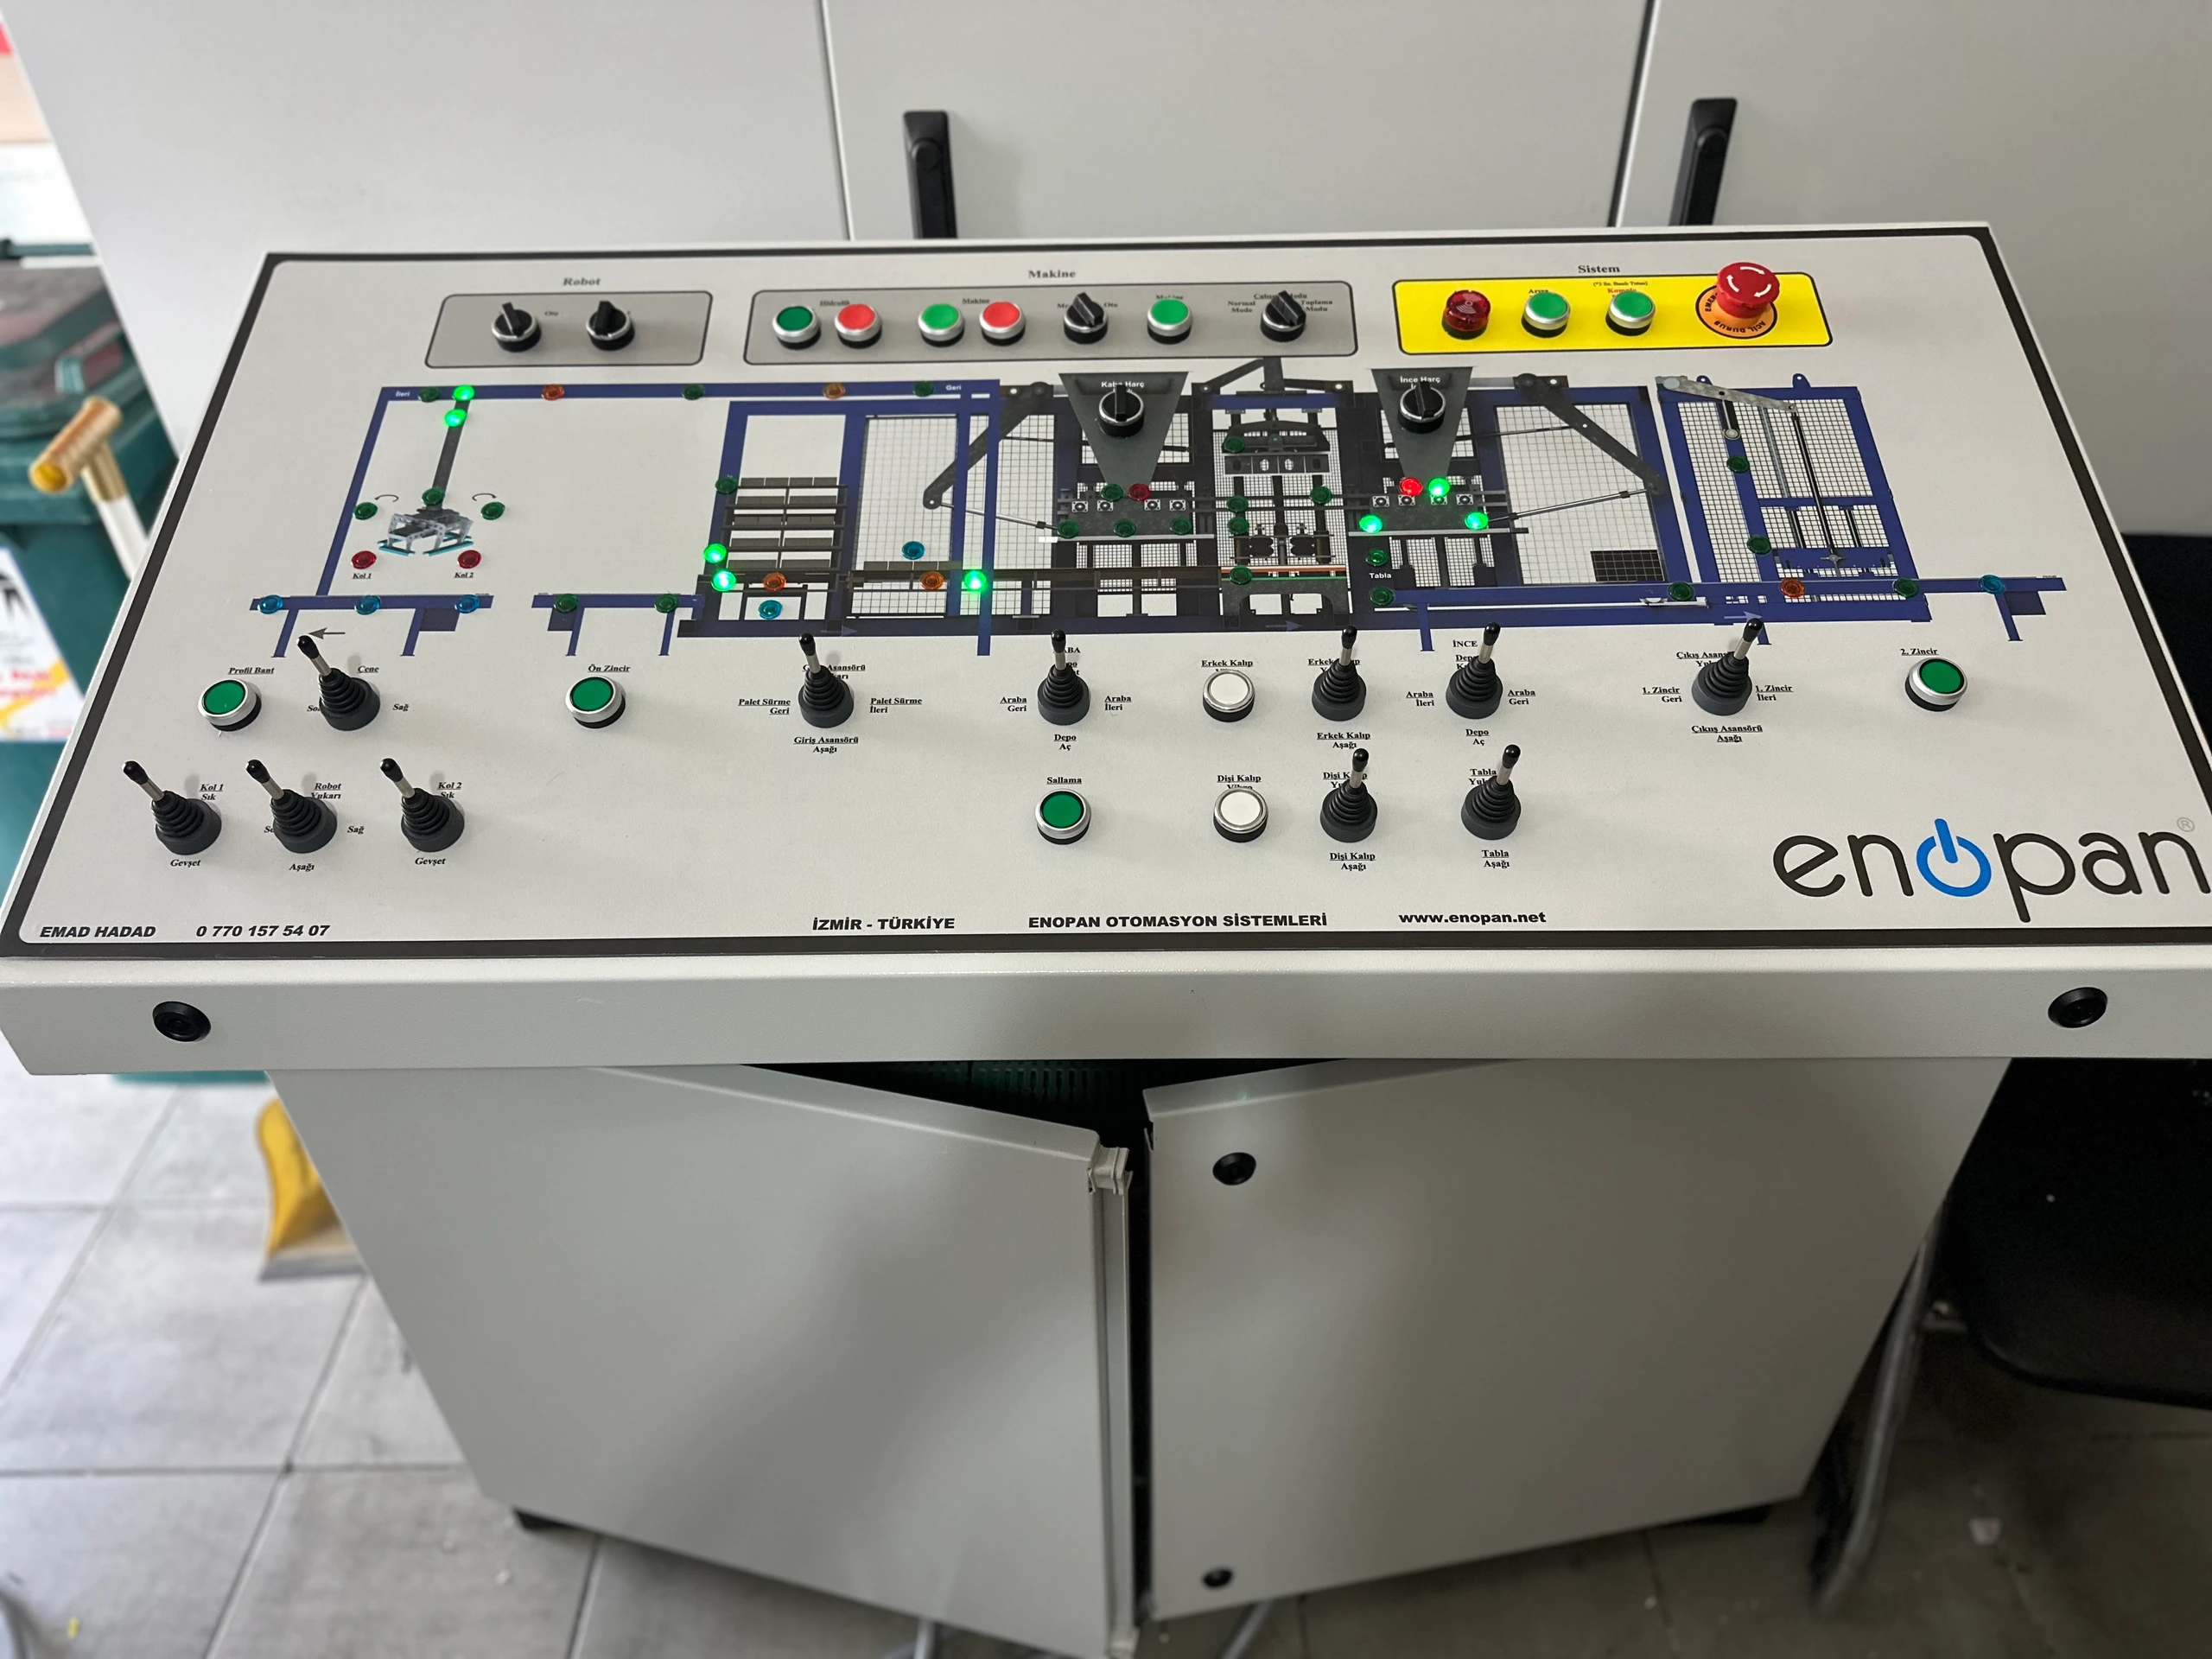
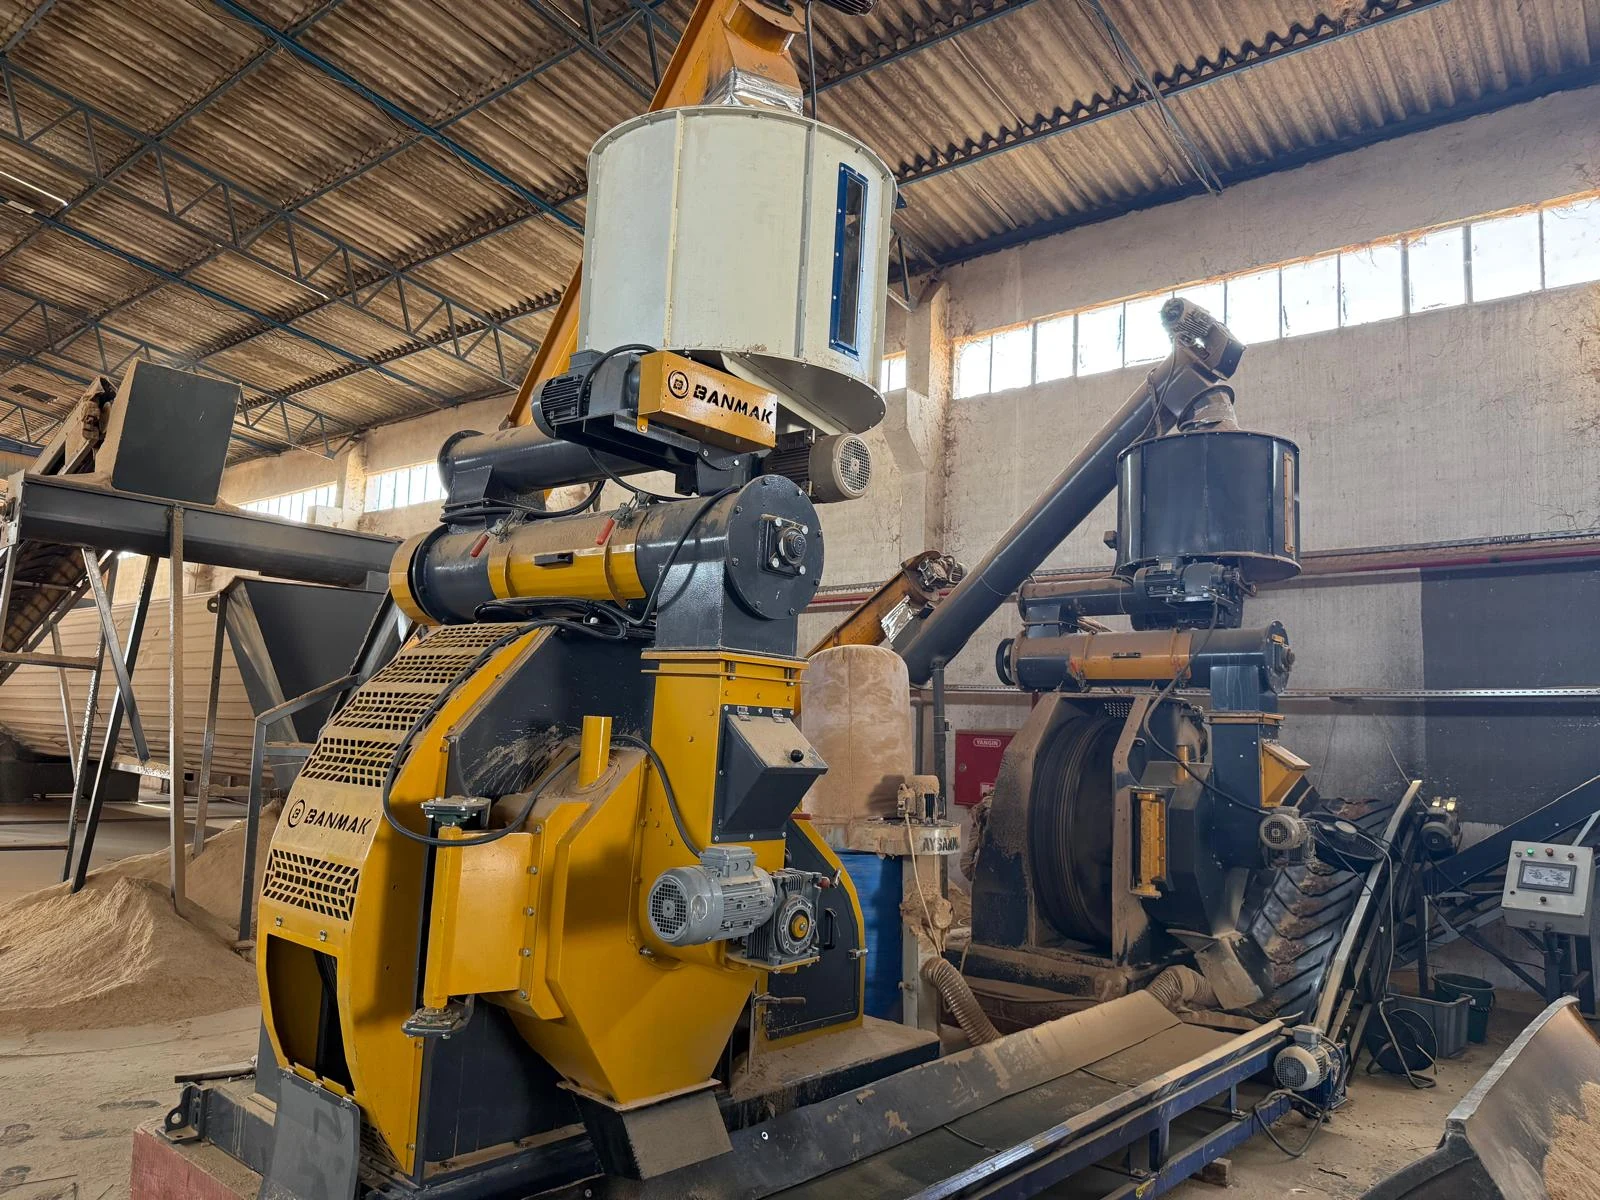
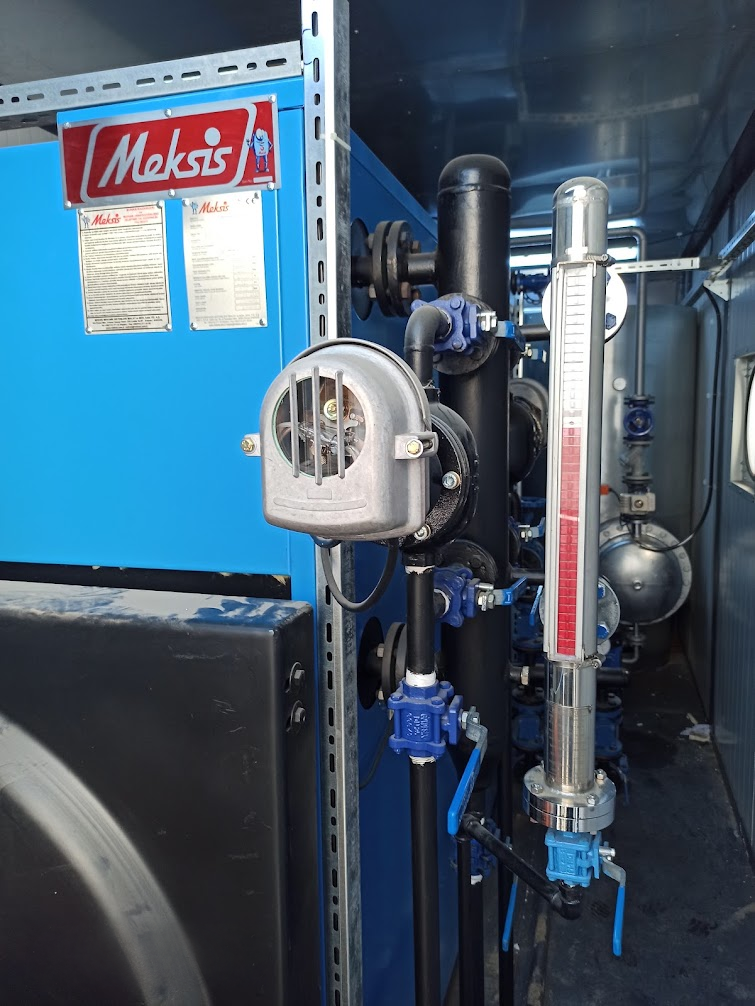
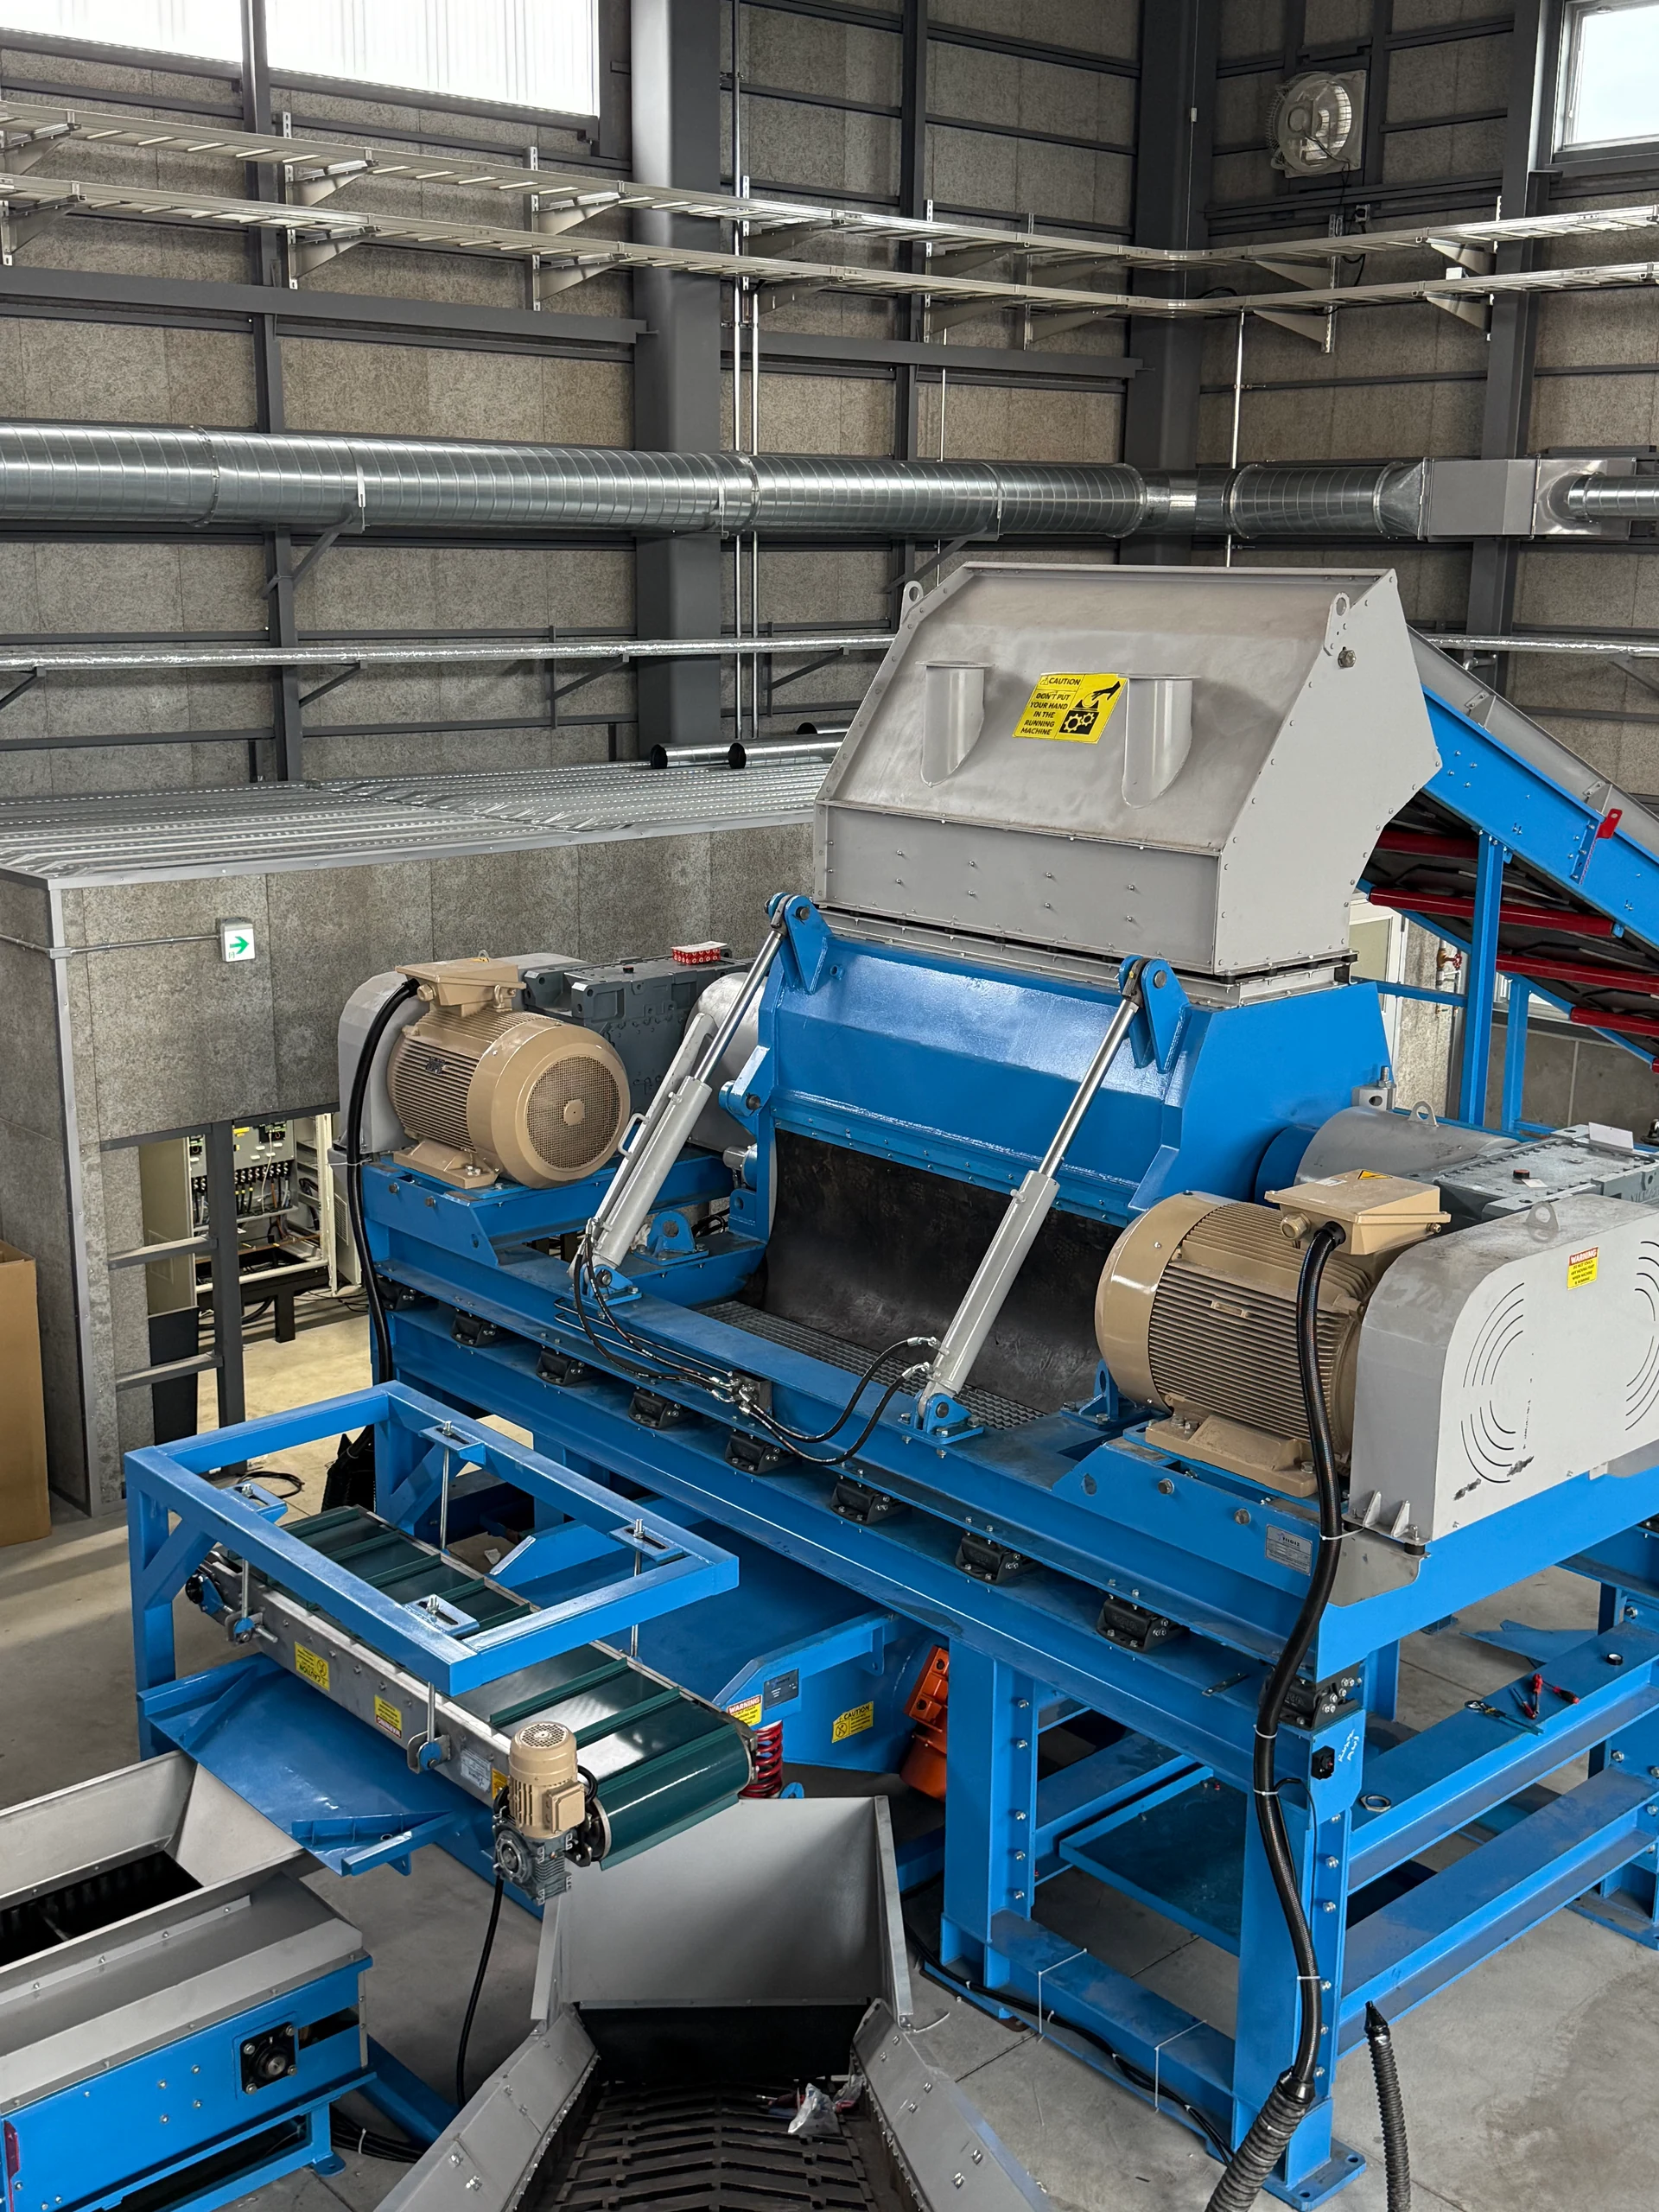
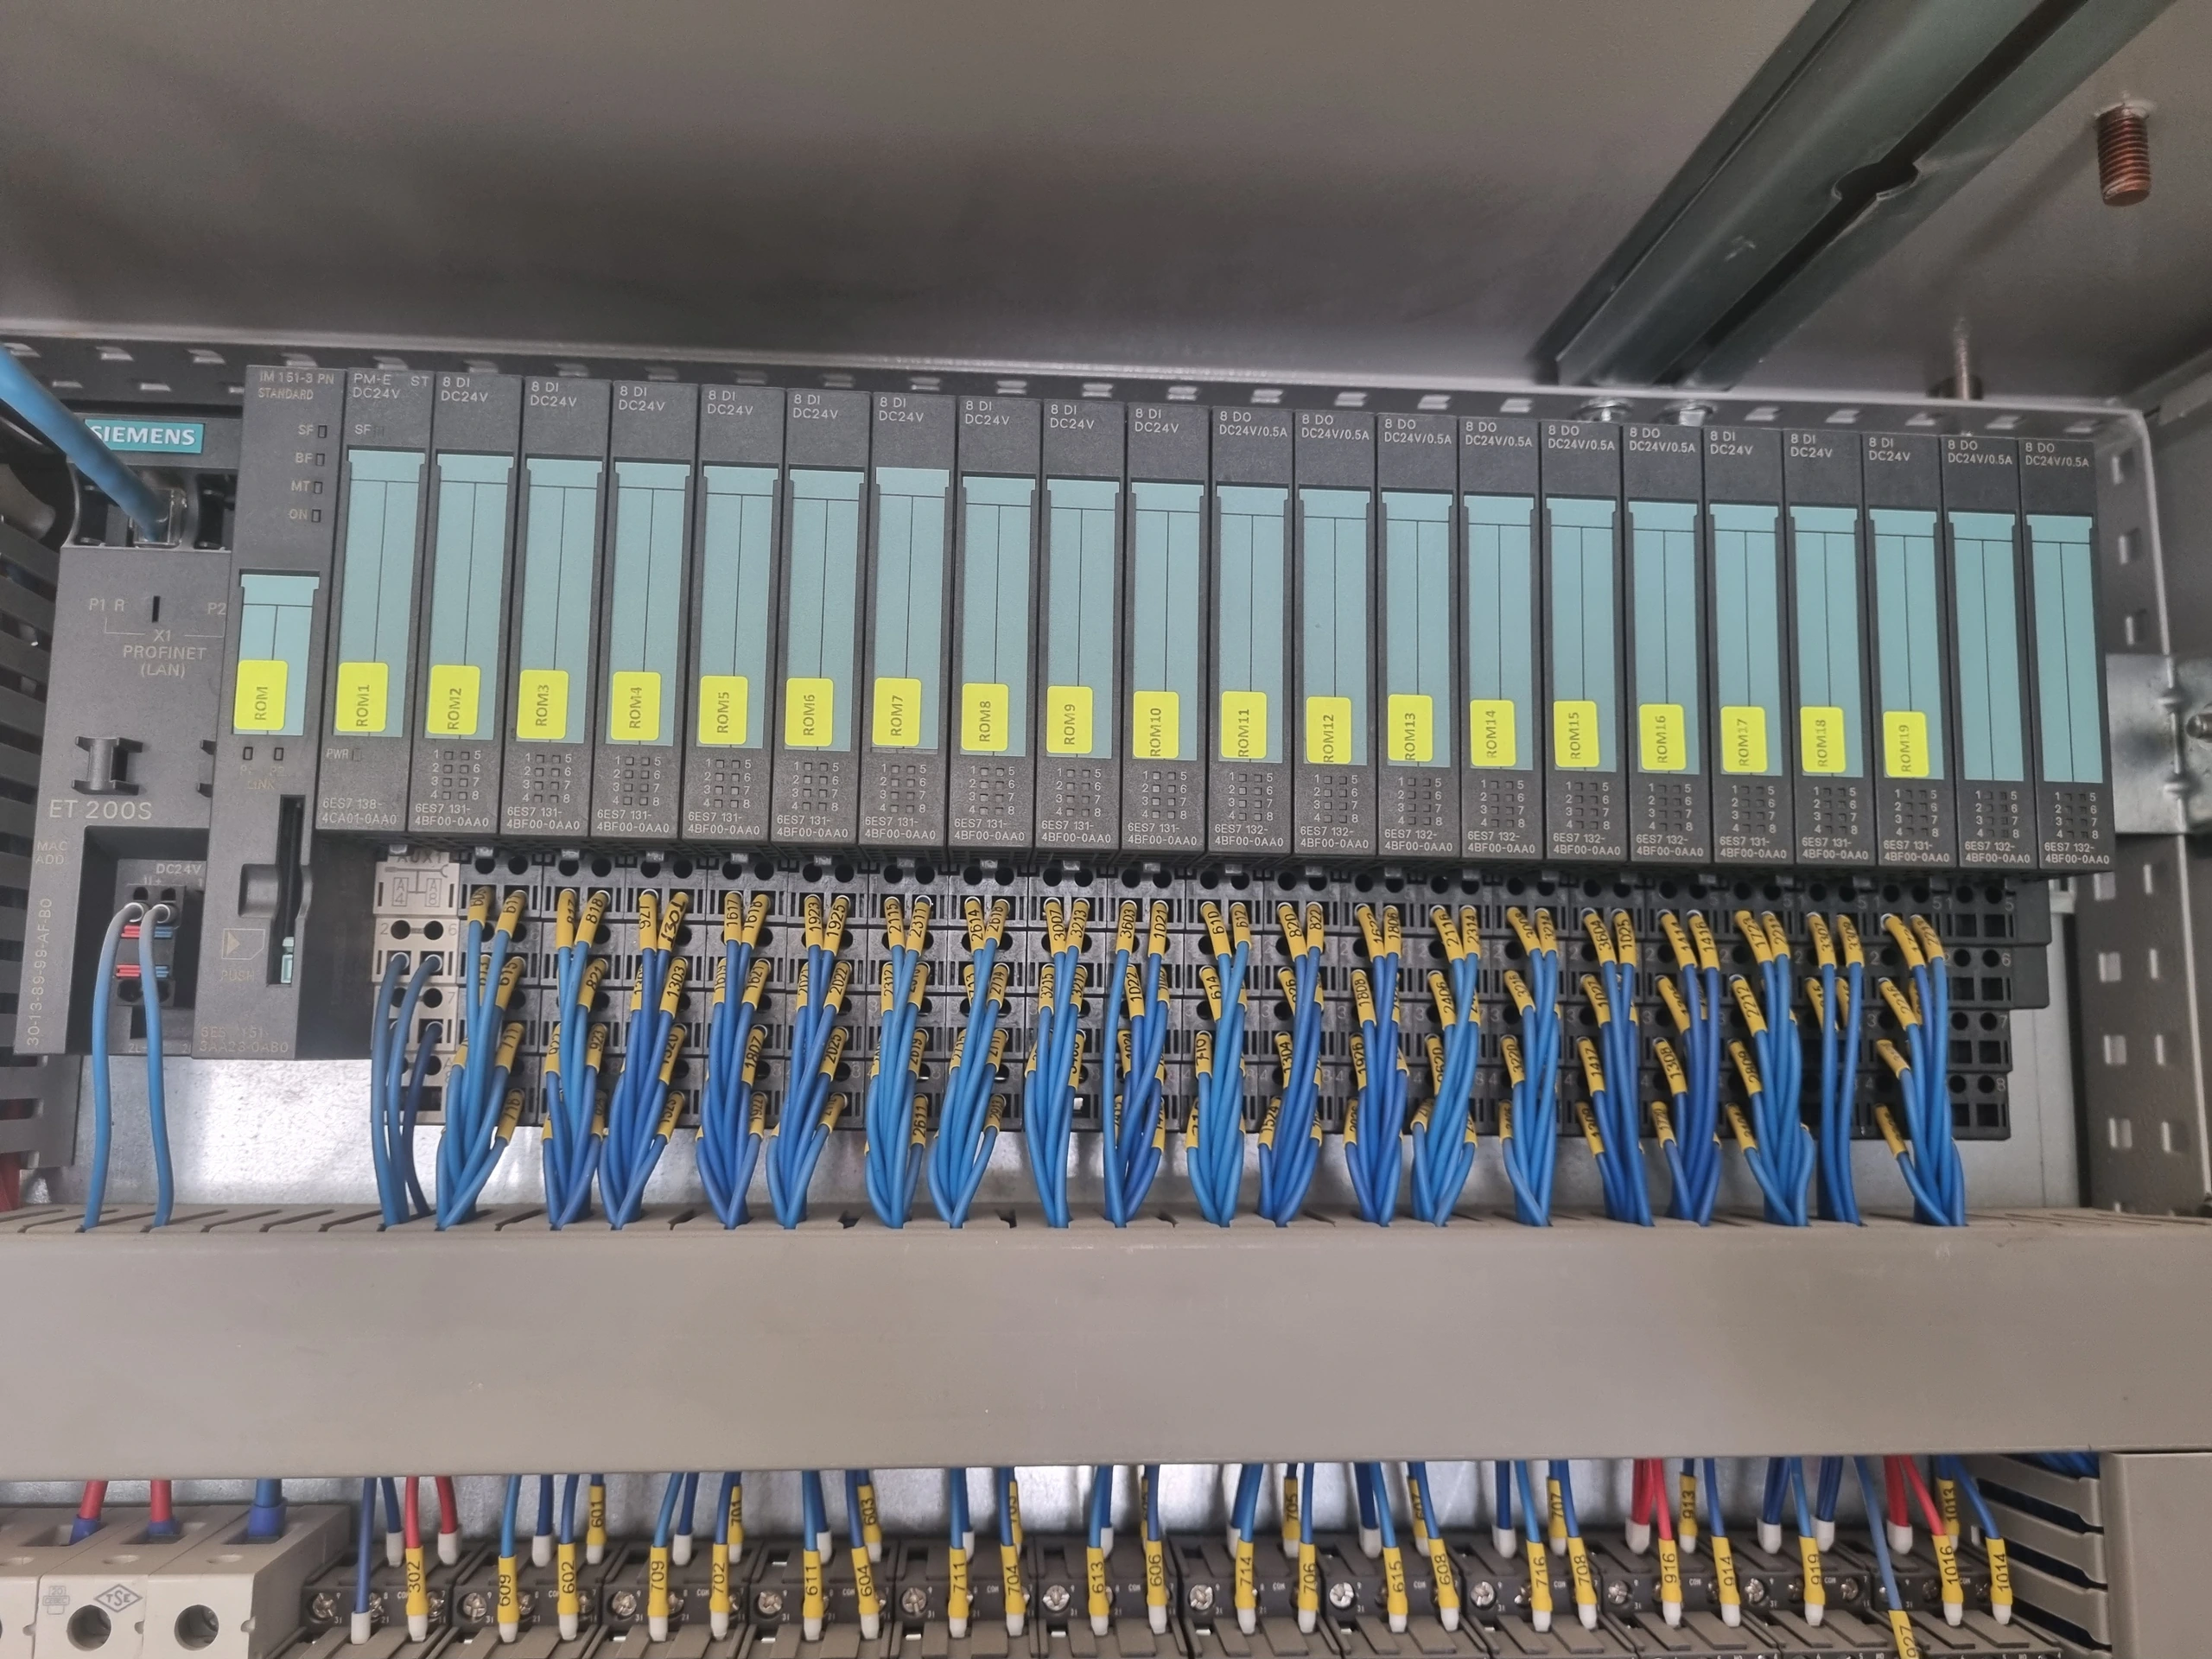
PLC software and HMI operator screens
We develop the PLC program according to the machine process sequence. We define sensor inputs, motor operating conditions and transitions between steps. Starting, stopping, automatic cycles and alarm states are considered within the same operating strategy.
The operator monitors machine status and changes operating parameters on the HMI screen. For recipe-based machines, the values used for the product are selected on screen. User permissions, parameters that can be changed and actions to be recorded are defined during project design.
- Process sequencing and automatic cycle control.
- Monitoring temperature, pressure, level and speed information.
- Displaying status, parameters and alarms on the operator screen.
Panel, motor and drive integration
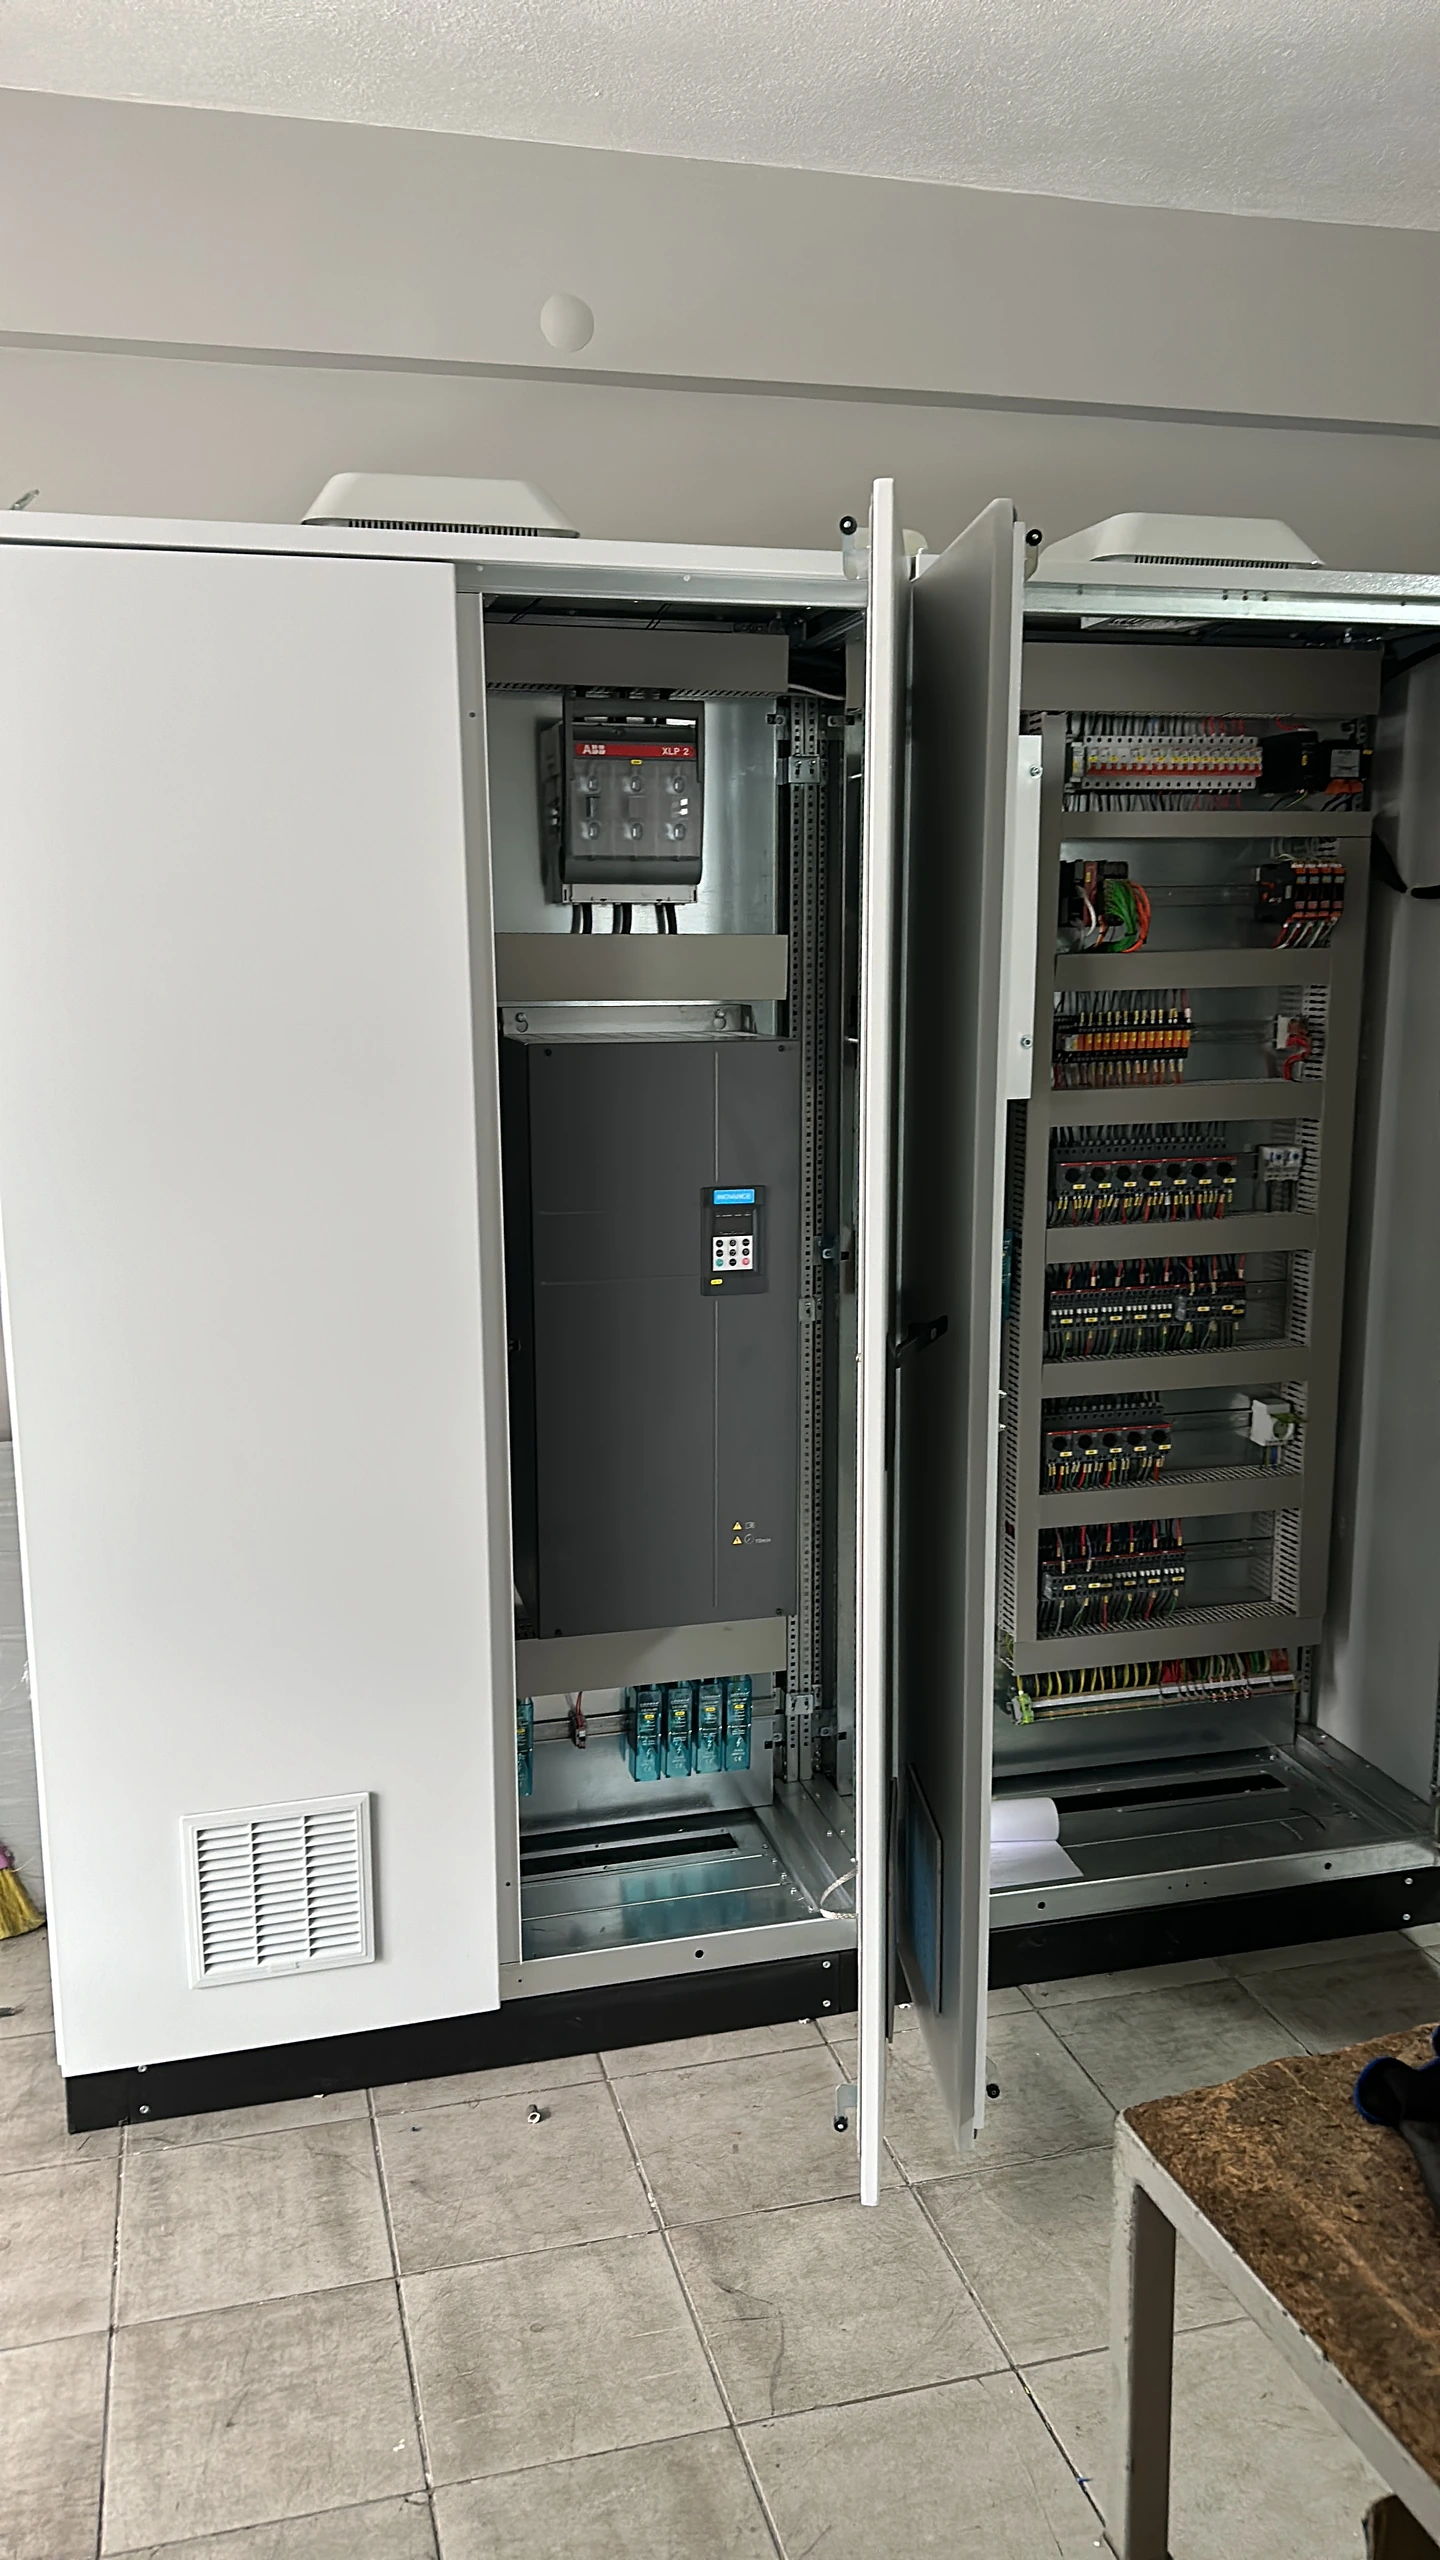
We assess machine sensors, motors and control hardware together with the electrical design. Connections and communications between the PLC, HMI and drives are arranged according to this equipment list. Panel work is scoped according to the requirements of a new installation or changes to an existing panel.
We handle servo, stepper motor and inverter drive integration according to the hardware used by the machine. The control strategy defines which motor runs in each operation, where speed settings are adjusted and how drive status is shown to the operator.
Automation retrofits for existing machines
For a retrofit, we first examine existing PLC/HMI details, program backups, electrical drawings and panel connections. We assess whether the requested change can be met through software, screen upgrades, or hardware and wiring work.
Describing the existing sequence together with the intended new behaviour clarifies the retrofit scope. For example, an operator parameter change, an unclear alarm or a drive replacement is considered separately. Modified functions are checked on the machine during commissioning.
We convert existing relay control systems to PLC and HMI control. The conversion considers the machine operating sequence, field connections and operator screens together.
Production monitoring, remote access and technical service
We define the data to be displayed and reported for production counts, operating times and alarm history. Live machine status and historical records require different screens and reports; we define the required information together when preparing the quotation scope.
We provide remote monitoring, control and report access from a phone or computer. The screens and remote control functions are defined according to the machine infrastructure. For technical service, we connect through the customer's computer or a remote access device when the customer provides internet access. The assessment distinguishes software review and fault analysis from work requiring on-site measurement or intervention.
Engineering, commissioning and handover
For a new machine, the operating strategy, equipment list, panel and operator screens are engineered together. On-site checks cover sensor input acquisition, motor and drive commands, process sequence and alarm notifications. These checks are scoped according to machine equipment and software functions.
PLC/HMI program backups, electrical drawings, an operating manual and operator training are included in our standard handover. Training covers screen use, parameters and reading alarm information.
Frequently asked questions
What information is needed for a machine automation retrofit?
Share the machine's function, existing PLC/HMI and drive details, panel photographs and the change you need. Available program backups, electrical drawings and fault information help with the technical assessment.
Can only the HMI screen or PLC software be upgraded?
The scope is defined after examining existing hardware, communications and program access. Some changes can be met through software or screens; others require modifications to hardware, panels and field connections.
Share your machine automation requirements
Describe the operating sequence of your new machine or the functions you want to change in your existing system. We can assess PLC, HMI, panels, drives and commissioning together.